
As high-grade copper resources become increasingly limited, the processing of low-grade copper ore is receiving more attention. However, ore grade alone does not determine the processing route. Copper mineralogy, oxidation state, mineral liberation, gangue composition, and the association between valuable minerals all influence how copper can be recovered.
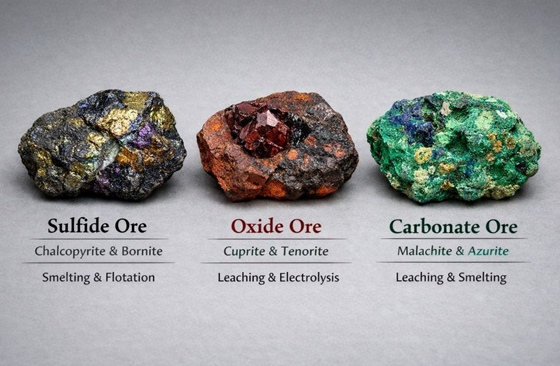
For many sulfide copper ores, the basic route involves crushing, grinding, and froth flotation. Low-grade oxide ores with suitable leaching characteristics may be treated by leaching followed by solvent extraction and electrowinning (SX-EW). Mixed or complex ores may require combined flowsheets.
The key to improving copper recovery is not simply increasing grinding fineness or reagent dosage. Instead, the processing conditions need to be matched with the characteristics of the ore, while copper losses are evaluated and controlled at each stage.
Low-grade copper ores can contain different copper minerals, including sulfide minerals such as chalcopyrite, chalcocite, and bornite, as well as oxide minerals such as malachite, azurite, and chrysocolla.
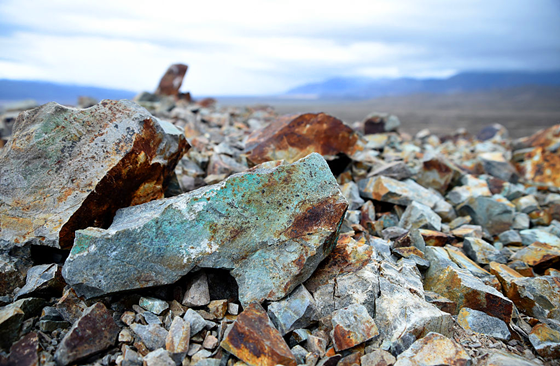
Their processing behavior can vary significantly. Some ores require finer grinding to achieve sufficient liberation between copper minerals and gangue. However, excessive grinding can generate large amounts of fine particles and slimes, which may reduce flotation efficiency. In other ores, copper minerals may already be sufficiently liberated at a coarser size, making unnecessary fine grinding an inefficient use of energy.
Therefore, the first step is to understand the ore rather than applying a fixed particle size or reagent scheme.
Low-grade copper ore is processed according to its mineralogy, oxidation state, liberation characteristics, gangue composition, and beneficiation response. Sulfide ores may be treated by crushing, grinding, and froth flotation, while suitable oxide ores may be processed by leaching followed by solvent extraction and electrowinning (SX-EW). Mixed or complex ores may require combined flowsheets. Mineralogical analysis and beneficiation testwork are normally used to determine the appropriate processing route and operating conditions.
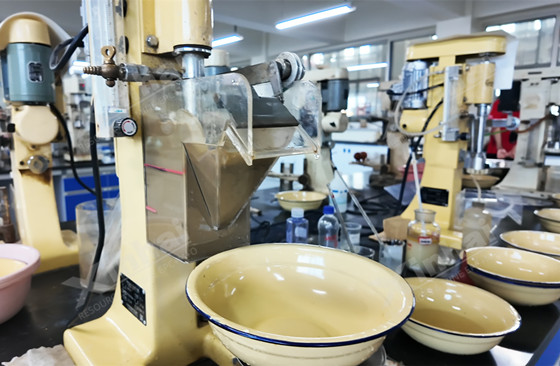
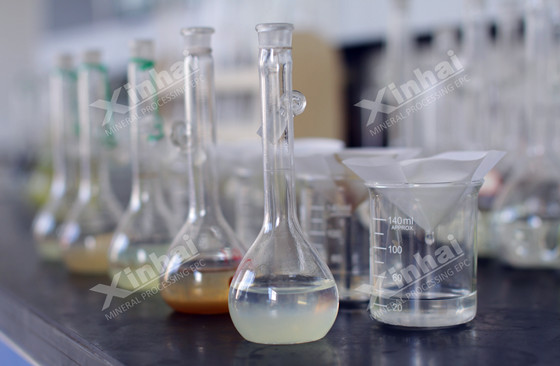
(copper flotation test)
Ore Characteristics | Potential Processing Route |
Sulfide copper minerals with good flotation response | Crushing → Grinding → Flotation |
Low-grade oxide copper ore with suitable leaching characteristics | Crushing → Leaching → SX-EW |
Mixed oxide-sulfide copper ore | Flotation + Leaching or other combined routes |
Complex polymetallic copper ore | Differential flotation, bulk flotation, or combined flowsheets |
Fine or unevenly disseminated copper minerals | Optimized grinding + flotation, potentially with stage grinding or stage separation |
These routes should be regarded as process options rather than fixed standards. Laboratory and pilot-scale testwork is normally required to determine the most suitable flowsheet for a specific ore.
For more information on copper beneficiation methods, see Xinhai's Copper Ore Beneficiation resources.
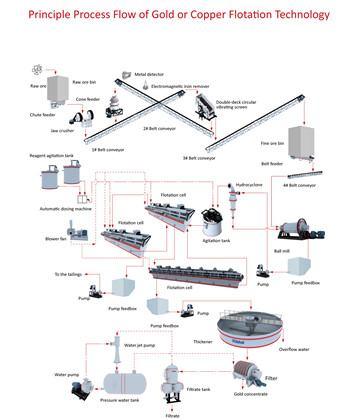
Froth flotation is an important beneficiation method for many sulfide copper ores. The typical process involves crushing and grinding to liberate copper minerals, followed by rougher, scavenger, and cleaner flotation.
The objective of grinding is not to achieve the finest possible particle size. It is to achieve sufficient mineral liberation while limiting unnecessary overgrinding.
Optimize Grinding for Mineral Liberation
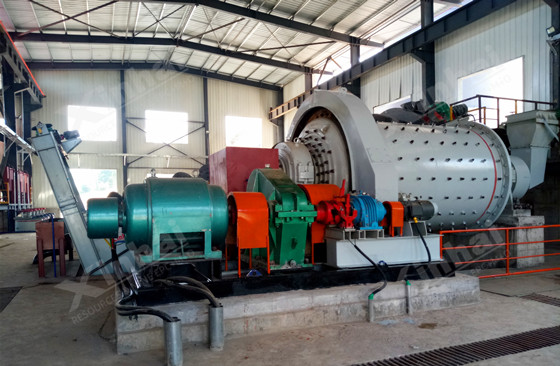
Grinding has a direct relationship with copper recovery because insufficient liberation can leave copper minerals locked with gangue.
However, finer grinding does not always mean higher recovery. Excessive grinding can increase the proportion of fine particles and slimes, which may interfere with particle-bubble attachment and affect flotation performance.
The appropriate grinding target should therefore be determined according to the mineralogical characteristics and liberation size of the ore.
Consider Stage Grinding and Stage Separation
When copper minerals show different liberation characteristics, stage grinding and stage separation may be considered.
Freely liberated copper minerals can be recovered at an earlier stage, while middlings or locked particles can be reground and treated again. This approach may help reduce unnecessary grinding of particles that are already sufficiently liberated.
The actual circuit configuration should be determined through beneficiation testing.
Optimize Flotation Conditions
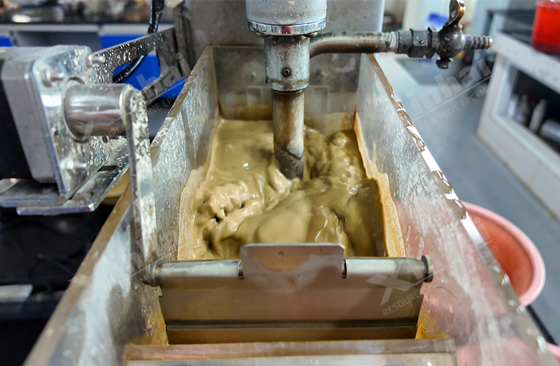
After grinding, flotation separates copper-bearing minerals from gangue based on differences in their surface properties.
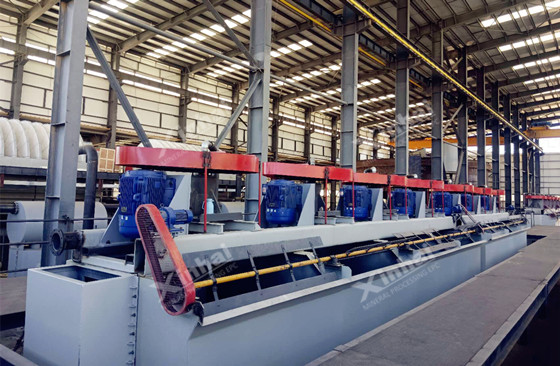
A typical copper flotation circuit may include:
Rougher Flotation → Scavenger Flotation → Cleaner Flotation
Collectors, frothers, pH regulators, depressants, and other reagents may be used depending on the mineralogy and separation requirements.
For a more detailed overview, see Xinhai's Copper Flotation Process.
Optimize the Reagent Scheme
Increasing reagent dosage does not necessarily improve copper recovery.
An excessive collector dosage may reduce selectivity, while an unsuitable frother or pH condition can affect froth stability and concentrate quality. The presence of pyrite, clay minerals, oxidized copper minerals, and other associated minerals can also change flotation behavior.
Therefore, reagent selection and dosage should be optimized through flotation tests rather than applied as a universal formula.
Control the Rougher, Scavenger and Cleaner Stages
Different flotation stages have different objectives.
Rougher flotation focuses on recovering as much valuable copper as practical into the rougher concentrate.
Scavenger flotation helps recover copper remaining in the rougher tailings.
Cleaner flotation improves concentrate grade by removing entrained or unwanted minerals.
Improving copper recovery requires a balance between recovery and concentrate quality. A circuit that focuses only on recovery may produce a concentrate with excessive impurities, while excessive cleaning may increase copper losses.
Low-grade oxide copper ores with suitable mineralogical and leaching characteristics may be processed by hydrometallurgical methods.
In a typical heap leaching route, crushed ore is placed on a prepared leach pad and contacted with a suitable leaching solution. The copper-bearing solution is collected and then processed through solvent extraction and electrowinning to produce copper cathodes.
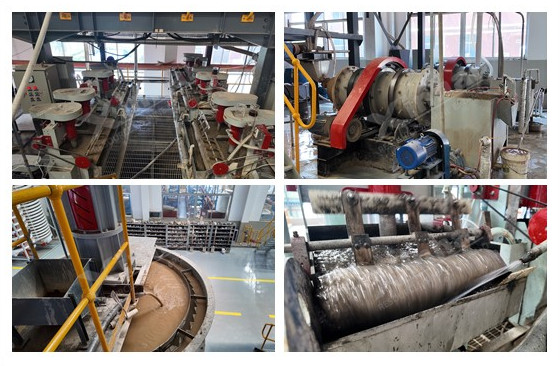
(oxide copper ore pilot-scale test)
Crushing → Heap Leaching → Pregnant Leach Solution → SX → EW → Copper Cathode
However, not every oxide copper ore is suitable for heap leaching. Mineralogy, acid consumption, permeability, gangue composition, copper mineral type, and leaching kinetics can all affect process performance.
Therefore, leachability testing is an important step before selecting a heap leaching process.
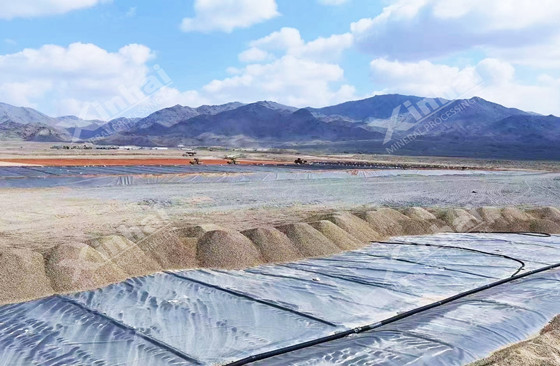
(copper ore heap leaching process)
Some deposits contain both sulfide and oxide copper minerals or are associated with other valuable metals.
For these ores, a single separation method may not be sufficient. Depending on the mineralogical characteristics, the flowsheet may combine flotation, leaching, gravity separation, or other beneficiation methods.
For polymetallic copper ores, possible flotation strategies include:
Differential flotation
Bulk flotation followed by separation
Selective flotation
Stage grinding and stage flotation
The selection depends on the association between copper and other valuable or gangue minerals.
Improving copper recovery requires systematic optimization of the entire beneficiation circuit, from mineralogical analysis and grinding to flotation and tailings management.
Identify the copper mineral types, distribution, liberation characteristics, grain size, gangue associations, and oxidation state. These factors determine the appropriate grinding and flotation strategy.
Set the grinding target according to the required liberation size, rather than simply increasing fineness. The objective is to achieve sufficient liberation while minimizing energy consumption and fine-particle losses.
Excessive grinding can generate fine copper-bearing particles that are difficult to recover by conventional flotation. Evaluate particle size distribution and flotation response to balance liberation with recovery.
Adjust the collector, frother, pH regulator, depressant, activator, dosage, conditioning time, and pulp conditions according to ore characteristics. Laboratory and pilot testwork can be used to establish the appropriate reagent regime.
Track copper distribution across rougher, scavenger, cleaner, and middling streams to identify major recovery losses. Depending on test results, circuit optimization may involve adjusting flotation stages, residence time, regrinding, or middlings treatment.
Analyze tailings to determine whether copper losses are related to insufficient liberation, locked particles, fine particles, poor selectivity, or incomplete scavenging. Where technically and economically justified, regrinding, additional flotation, or tailings reprocessing can be evaluated.
A practical example of ore-specific process design is the Yunnan 1,000 t/d Copper Mineral Processing Plant. The raw ore had a copper grade of 0.87%, with chalcopyrite, pyrite, tetrahedrite, and malachite as the main metal minerals, while quartz, calcite, dolomite, chlorite, sericite, and tourmaline were among the main gangue minerals. Based on the ore characteristics, Xinhai Mining Group adopted a closed-circuit grinding process followed by copper flotation, with one roughing, three scavenging, and three cleaning stages. The grinding fineness reached 75% passing 200 mesh.
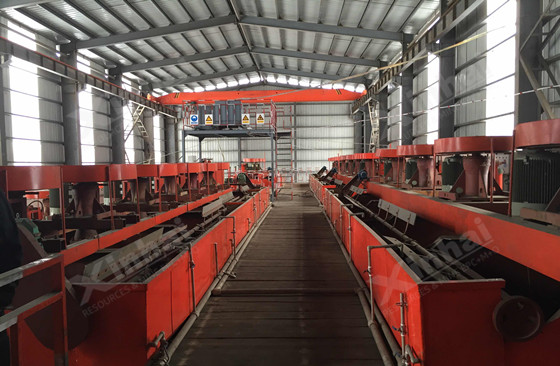
(Yunnan 1,000 t/d Copper Mineral Processing Plant)
The project produced a copper concentrate grading 23.00% Cu, with a reported copper recovery of 91.21%. This case illustrates why low-grade copper processing cannot rely on a fixed grinding size or flotation scheme: the flowsheet needs to be developed around the mineralogy, liberation characteristics, and beneficiation response of the specific ore.
There is no universal processing route for low-grade copper ore. Sulfide ores may be treated by flotation, while suitable oxide ores may be processed by leaching and SX-EW. Mixed and complex ores may require combined flowsheets. The appropriate route depends on mineralogy, liberation characteristics, oxidation state, gangue composition, and beneficiation test results.
Grinding is used to achieve sufficient liberation between copper minerals and gangue. However, excessive grinding can generate fine particles and slimes that may affect flotation. Therefore, the grinding target should balance mineral liberation and particle-size control.
Beneficiation testwork helps determine how the ore responds to grinding, flotation, leaching, or combined processing methods. Because copper deposits can differ significantly in mineralogy, liberation, gangue composition, and oxidation state, testwork provides a basis for developing and optimizing the flowsheet.
Share your project details and our engineers will get back to you shortly.
 CHAT
 MESSAGE